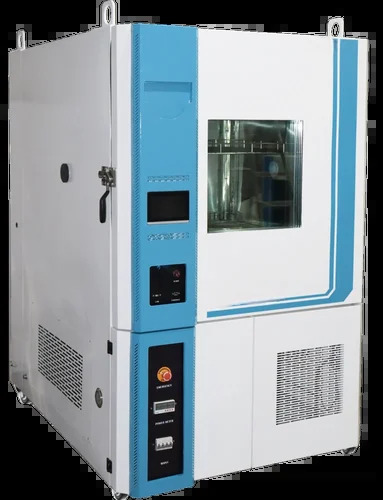
About 100L Humidity Walk In Chamber
Buy the highly sought-after 100L Humidity Walk In Chamber, a brilliant solution engineered for world-class professionals. This valorous chamber is designed for in-demand precision, featuring a 100-liter capacity and constructed from robust mild steel in a sleek rectangle shape. Its low power consumption and flexible voltage range (220-440V) make it remarkably efficient. Powered electrically, its ideal for quality control across pharmaceuticals, electronics, and materials science industries. From manufacturers to suppliers across India, this chamber is your ticket to reliable and consistent environmental testing. Try now for dependable results!
Versatile Usage and Industry Applications
The 100L Humidity Walk In Chamber is widely used by top-tier laboratories and production units in the pharmaceutical, electronics, and materials science sectors. Its primary use type is quality and environmental control testing, ensuring that products meet rigorous standards. This chamber supports testing processes under controlled humidity and temperature conditions, making it indispensable for stability studies, durability checks, and product validations across diverse industries.
Seamless Dispatch, Certifications, and Supply Capability
Our 100L Humidity Walk In Chamber is ready for exchange or handover at major Indian FOB Ports. Each unit is supplied with necessary certifications ensuring compliance with international safety and performance standards. With a world-class supply ability, we ensure the brisk dispatching and delivery of chambers to meet ongoing industrial demands. Rely on our efficient process and streamlined logistics for smooth procurement and deployment.
FAQs of 100L Humidity Walk In Chamber:
Q: How does the 100L Humidity Walk In Chamber support quality control processes?
A: The chamber enables precise humidity and temperature control, essential for simulating and evaluating real-world environmental conditions, thus ensuring product reliability and compliance in quality control tests.
Q: What industries can benefit from using this chamber?
A: Pharmaceutical, electronics, and materials science industries utilize the chamber for product testing, stability analysis, and environmental stress validation, enhancing their quality assurance protocols.
Q: Where can this chamber be dispatched or exchanged from?
A: The 100L Humidity Walk In Chamber is available for dispatch or exchange through major Indian FOB ports, supporting timely deliveries across the country and overseas.
Q: What certifications accompany the 100L Humidity Walk In Chamber?
A: Each unit comes with essential certifications that confirm adherence to international standards for safety, efficiency, and performance.
Q: What is the typical supply capacity and process for handover?
A: We maintain consistent supply capability, enabling swift processing, handover, and dispatching upon order placement, ensuring prompt fulfillment for industrial requirements.
Q: What are the benefits of choosing this world-class mild steel chamber?
A: Benefits include robust durability, low power consumption, flexible voltage compatibility, and versatile applications in multiple quality-driven industries.
 We'are Open: Mon - Sat 10:00 AM - 7:00 PM



 Send Inquiry


 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
